


Mould-making tools ·
Plan a craft mould's filling channels with a custom half-round sprue pattern
Position a printed positive sprue pattern on your mould's parting plane. Adjust its length, outlet span and channel size before downloading the STL.
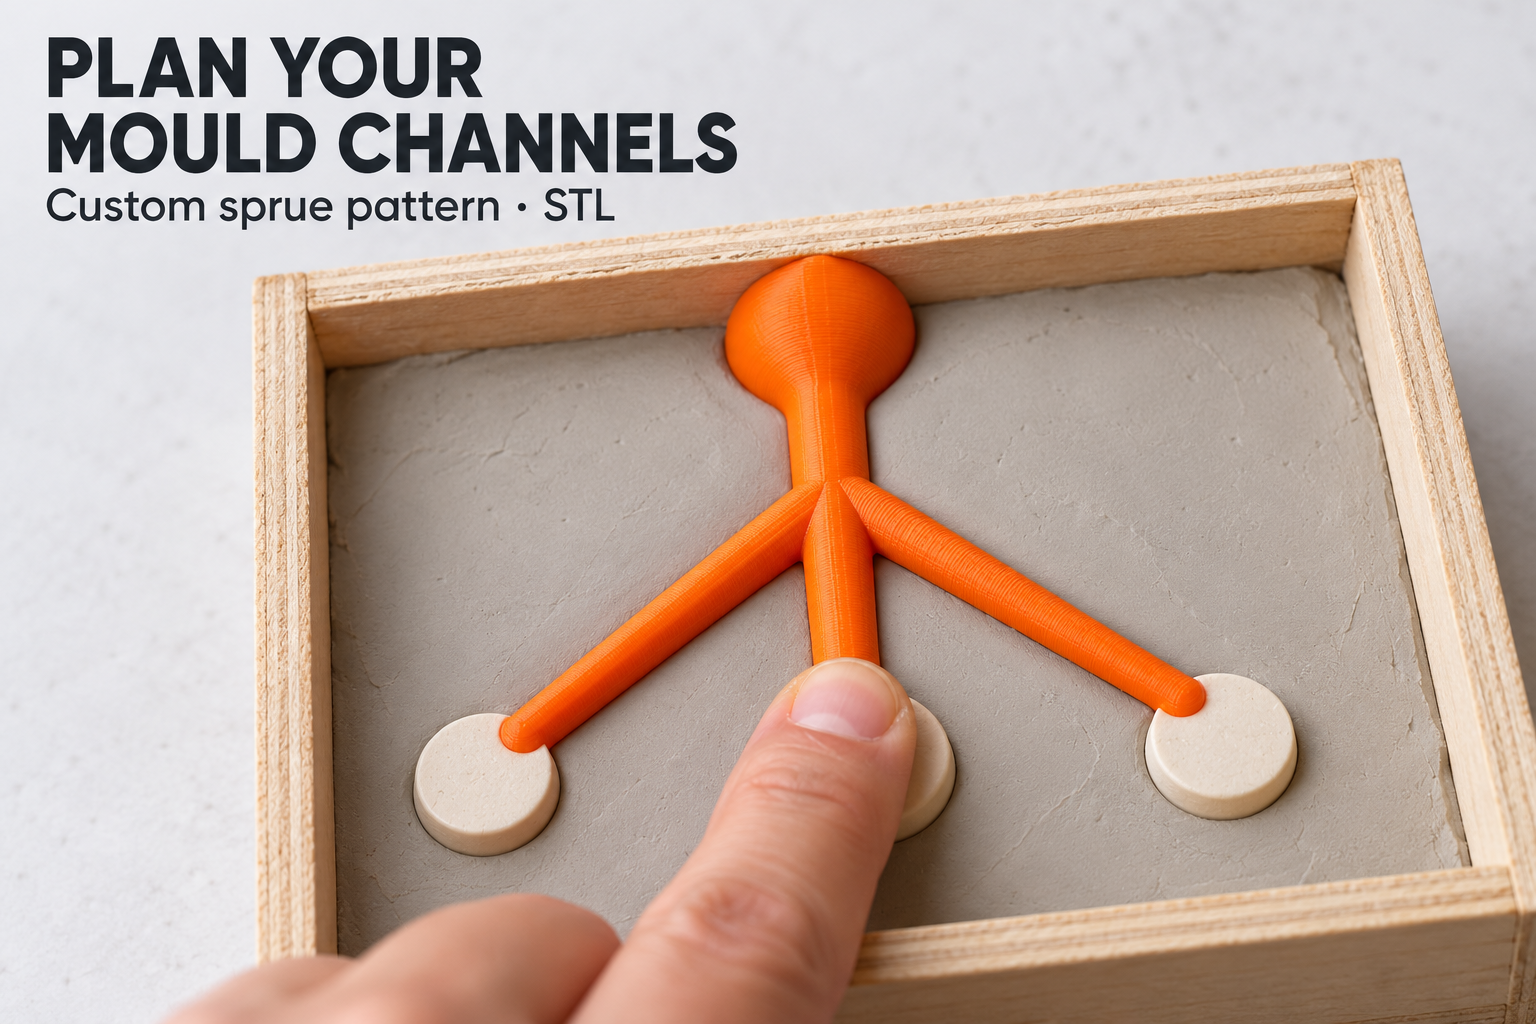
Lay out the feed paths before making the mould
For a small homemade craft mould, the route from the inlet to each cavity deserves as much planning as the objects being copied. This parametric sprue tree gives you a solid printed pattern with a flat back and three half-round branches. Place it on the prepared parting plane so its shape can be reproduced as negative channels in the mould material.
If you are looking for a sprue tree STL sized around your own layout, you can adjust the main dimensions before downloading it. The printed piece is a removable positive pattern. It does not remain as a hollow funnel carrying the casting material through its plastic body.
Set the length, spread and channel diameter
The inlet-to-outlet distance is adjustable from 40 to 100 mm, with a 60 mm default. The outer outlet span can range from 30 to 90 mm, also initially 60 mm. Use these dimensions to place the three branch ends where your intended gates will meet the mould cavities.
Branch channel diameter ranges from 3 to 8 mm, initially 4 mm. The inlet head diameter is adjustable from 14 to 28 mm, with 18 mm as the starting value. Select these for your own material and mould layout; the model does not calculate an optimal filling rate.
The branch-point setting is a fraction of the inlet-to-outlet length, between 0.3 and 0.6. The default 0.45 places the junction at 45 percent of that distance. At a 60 mm length, that is 27 mm from the inlet reference. Moving the junction changes where the outer branches spread without changing the meaning of the overall length.
Use the flat face on the parting plane
Inspect the print for rough edges and make sure its back can sit flat. Position the pattern on the prepared parting plane, with the inlet connected to the planned outside access and each branch end connected to its intended gate. Check these contacts before applying mould material: a small gap can leave an interrupted path.
After forming the mould, remove the pattern using a release method appropriate to your chosen materials. Its half-round surfaces leave corresponding negative impressions. How those impressions meet the other mould half depends on your complete design. The printed tree alone does not define alignment features, closure, venting or the final cavity arrangement.
Test the complete cold-process setup
Provide suitable vents and check compatibility between the pattern, mould material, release treatment and casting material. Make a small trial with the actual system before relying on the layout. Bubble-free filling is not guaranteed. This pattern is intended for suitable cold-process craft and model-making materials, not molten metal or hot casting.
The image is an AI visualization of a dry layout stage. Geometry has been digitally checked without a claimed physical test print; the mould box and master objects are not included. Configure your custom half-round sprue pattern and purchase the STL to print a layout matched to your next mould.
Next step